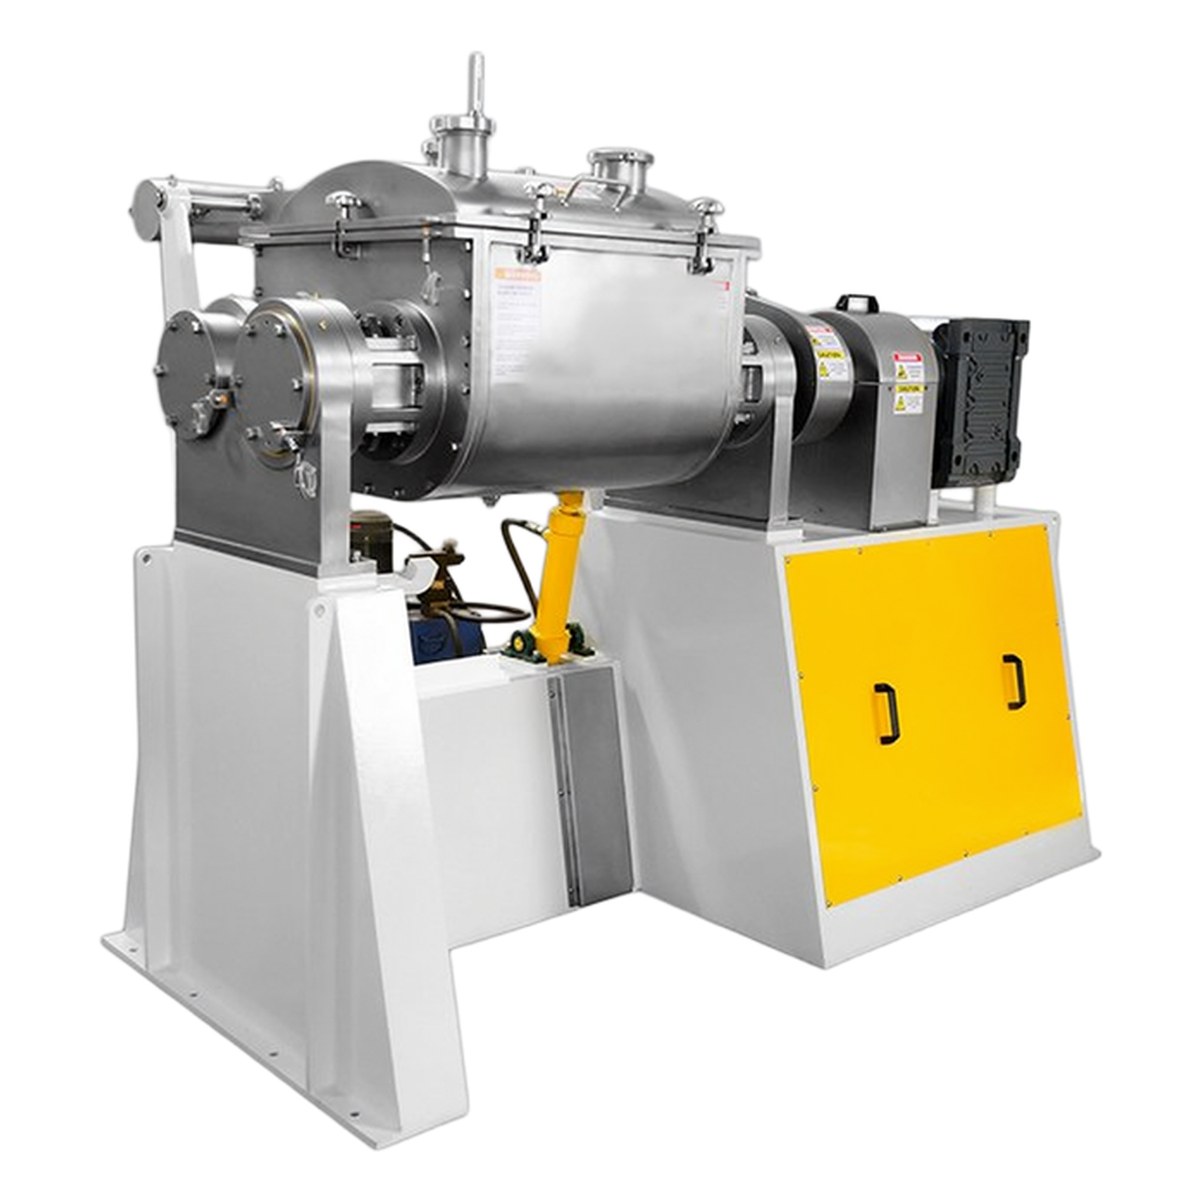
Kneader
1. Product Overview
1.1 General Description
The kneader is key equipment for mixing, reacting and drying high-viscosity materials in the chemical, food and pharmaceutical industries. Two intermeshing Sigma- or Z-shaped blades rotate in opposite directions at different speeds inside a W-shaped trough, exerting strong compression, shear, folding and stretching on the material to achieve uniform mixing in a short time. A kneader handles viscosities up to several million mPa·s and is a purpose-built mixer that conventional agitators cannot replace. Modern kneaders adopt variable-frequency drives and PLC control to support forward/reverse rotation, vacuum operation and heating/cooling cycles. They are widely used for high-viscosity materials such as silicone rubber, sealants, carbon compounds, battery pastes, food fillings and pharmaceutical ointments.
1.2 Key Features
- Twin Sigma/Z-blade design delivers strong shear and high mixing uniformity
- Blade speed ratio 1:1.2–1:1.5 creates intense compression and folding
- Handles extremely high-viscosity materials (100k–5,000k mPa·s)
- W-shaped trough leaves no dead zone and discharges cleanly
- Variable-frequency drive allows stepless speed adjustment for different materials
- Optional vacuum system down to -0.095 MPa
- Jacketed trough for steam/thermal-oil heating or cooling-water cooling
- Hydraulic trough tilting for easy, clean discharge
- Product-contact parts in SS304/316L stainless steel
- PLC + HMI control stores multiple process recipes
1.3 Document Scope
This specification covers the kneader's design principle, performance parameters, system classification, core component selection, application fields, design standards and certifications, optional custom configurations, warranty terms, packaging and delivery, and the information required for inquiry. It serves as a comprehensive reference for procurement selection and engineering communication.
2. Working Principle
2.1 Kneader Process Flow
Complete workflow: feeding → low-speed pre-mix → high-speed kneading → vacuum de-aeration → temperature-controlled reaction → trough tipping/discharge → cleaning. The two blades rotate in opposite directions at different speeds; on meshing, material is compressed, sheared and folded, and on separating it is stretched and dispersed. The Sigma blade suits medium-viscosity materials, the Z-blade suits ultra-high-viscosity materials. Blade-to-wall clearance is 2–5 mm. Vacuum-type kneaders are fitted with a vacuum system that pulls below -0.095 MPa during mixing to remove air bubbles and volatiles.
3. System Classification
| | | | |
|---|
| Lab type | NH-5, NH-10 | 5–10 L | R&D / lab trial | Compact |
| Pilot type | NH-50, NH-100 | 50–100 L | Pilot production | Vacuum & temp. control |
| Production type | NH-200, NH-500 | 200–500 L | Standard production | Hydraulic tipping |
| Large production type | NH-1000, NH-2000 | 1000–2000 L | Large-scale production | Dual-drive PLC |
4. Technical Parameters
4.1 Main Technical Parameters
| NH-5 | NH-50 | NH-100 | NH-200 | NH-500 | NH-1000 | NH-2000 |
|---|
| Working volume (L) | 5 | 50 | 100 | 200 | 500 | 1000 | 2000 |
| Total volume (L) | 8 | 80 | 160 | 320 | 800 | 1600 | 3200 |
| Motor power (kW) | 2.2 | 7.5 | 11 | 15 | 22 | 37 | 55 |
| Blade type | Sigma | Sigma/Z | Sigma/Z | Sigma/Z | Sigma/Z | Sigma/Z | Sigma/Z |
| Fast blade speed (rpm) | 35 | 35 | 32 | 30 | 28 | 25 | 22 |
| Slow blade speed (rpm) | 25 | 25 | 22 | 20 | 18 | 16 | 14 |
| Speed ratio | 1:1.4 | 1:1.4 | 1:1.45 | 1:1.5 | 1:1.55 | 1:1.56 | 1:1.57 |
| Discharge | Manual tipping | Manual tipping | Hydraulic tipping | Hydraulic tipping | Hydraulic tipping | Hydraulic tipping | Hydraulic tipping / bottom outlet |
| Vacuum (MPa) | -0.095 | -0.095 | -0.095 | -0.095 | -0.095 | -0.095 | -0.095 |
| Jacket pressure (MPa) | 0.3 | 0.3 | 0.3 | 0.3 | 0.3 | 0.3 | 0.3 |
4.2 Dimensions and Weight
| | | | | |
|---|
| NH-5 | 800 | 600 | 1000 | 200 | 0.5 |
| NH-50 | 1200 | 900 | 1400 | 800 | 1.1 |
| NH-100 | 1400 | 1000 | 1500 | 1200 | 1.5 |
| NH-200 | 1600 | 1100 | 1600 | 1800 | 1.8 |
| NH-500 | 2000 | 1300 | 1800 | 3200 | 2.6 |
| NH-1000 | 2400 | 1500 | 2000 | 5500 | 3.6 |
| NH-2000 | 3000 | 1800 | 2300 | 9000 | 5.4 |
5. Applications
| | | |
|---|
| Silicone rubber | HTV/RTV silicone rubber | Vacuum de-aeration | Silicone sealant |
| Sealant | Silicone / polysulfide sealant | Bubble-free | Construction sealant |
| Battery | Li-ion electrode paste | Vacuum de-aeration, no contamination | Anode/cathode paste |
| Food | Chocolate / dough / filling | FDA compliant | Chocolate mass |
| Pharma | Ointment / suppository / paste | GMP compliant | Ointment base |
| Carbon | Carbon paste / electrode paste | High-temp heating | Graphite electrode paste |
6. Core Component Selection
| | | |
|---|
| Kneading blades | Compression, shear, folding & mixing | SS316L | Sigma / Z selection |
| Trough | Holds material, W-shaped vessel | SS304/316L | Wall thickness per pressure calc. |
| Drive system | Drives blade rotation | Gearbox + reducer | Dual or single motor split |
| Sealing | Prevents shaft-end leakage | PTFE / mechanical seal | Vacuum type needs mech. seal |
| Tipping mechanism | Tilts trough for discharge | Hydraulic cylinder + hinge | Tilt angle 110–120° |
| Jacket | Heating / cooling | SS304 | Steam 0.3 MPa or thermal oil |
| Vacuum system | Removes bubbles & volatiles | Water-ring pump + condenser | Limit -0.095 MPa |
| Control system | Coordinates operation | PLC + HMI | Recipe storage & data log |
7. Design Standards and Certifications
| | | |
|---|
| GB/T standards | Design & manufacture | Fully compliant | Type-test report |
| GMP (cGMP) | Design, manufacture, docs | Fully compliant | GMP certificate |
| ISO 9001:2015 | Quality management | Certified | ISO 9001 certificate |
| CE | Machinery safety / EMC | Optional | CE declaration |
| FDA | Food / pharma grade | Optional | FDA compliance docs |
8. Custom Optional Configurations
| | | | |
|---|
| 1 | Blade type | Sigma / Z / fishtail / combined | Sigma | Combined +1–2 wks |
| 2 | Heating | Electric / steam / thermal oil | Electric | Thermal oil +2 wks |
| 3 | Discharge | Tipping / screw / bottom valve | Hydraulic tipping | Screw +2–3 wks |
| 4 | Vacuum | Standard / high / none | Standard | High vacuum +1–2 wks |
| 5 | Control | Push-button / PLC / DCS | PLC + HMI | DCS +3–4 wks |
| 6 | | SS304 / 316L / Hastelloy | SS304 | Hastelloy +4–6 wks |
| 7 | Explosion-proof | Standard / ExdIIBT4 | Standard | Ex-proof +2–3 wks |
| 8 | Cleaning | Manual / CIP / combined | Manual | CIP +2 wks |
9. Material Property Requirements
| | |
|---|
| Working temp. | -40~250℃ | Depends on seal & material |
| Corrosiveness | Weak–medium | Strong corrosion needs 316L or lining |
| Ex-proof req. | Per site | Zone1/Zone2 grades |
10. Warranty Terms
| | | |
|---|
| Main equipment | 12 months | All components | From commissioning acceptance |
| Extended warranty (opt.) | 24 months | Same as standard | Purchase at order |
| Wear parts | 6 months | Seals, bearings, etc. | Normal wear excluded |
11. Packaging and Delivery
| |
|---|
| Standard lead time | 6–10 wks after PO |
| Custom lead time | 10–16 wks |
| Incoterms | FOB Shanghai / CIF / DAP |
| Packing | Export wooden case |
| Shipping | Container or break-bulk |
12. Information Required for Inquiry
| | |
|---|
| 1 | Material name & properties | Name / viscosity / solids / corrosiveness |
| 2 | Working volume | L/batch or kg/batch |
| 3 | Blade preference | Sigma / Z / fishtail |
| 4 | Heating/cooling | Electric / steam / thermal oil / cooling water |
| 5 | Vacuum req. | Vacuum level required? |
| 6 | Discharge | Tipping / screw |
| 7 | Material | SS304/316L |
| 8 | Ex-proof grade | Standard / ex-proof |
| 9 | Control | PLC/HMI/DCS |
| 10 | Install cond. | Building height / load / power |